CNC turning
Complex profiles and multiple features in one set-up. Used for samples, short and medium runs, and parts that change often.
Ø5–100 mm · ±0.05 mmRod comes from approved mills. Forging, turning, stamping, secondary operations, plating and packing happen in our plant in Jamnagar; material tests (composition, strength) go to an outside lab.
Each part is routed to the process that gives the lowest cost at its volume.
Design for cost: with each quote we suggest where cost can come out, such as forging instead of machining from bar, a special bar profile to cut operations, or relaxing non-critical dimensions. You approve every change.
Complex profiles and multiple features in one set-up. Used for samples, short and medium runs, and parts that change often.
Ø5–100 mm · ±0.05 mm
Bar-fed cam-operated automats for long runs of small and medium parts at the lowest piece price.
bar-fed
Near-net brass forgings for bodies, tees and manifolds, then machined to finish. Less material and fewer operations than machining from bar.
25 g – 1.0 kgshot-blasted · natural · bright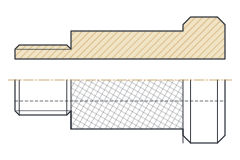
Single-operation machines, built in-house with our own fixtures, for turning, drilling, threading and milling on large batches of repeat parts. They take manual handling, and with it errors, out of repeat jobs.
drill · tap · mill · slot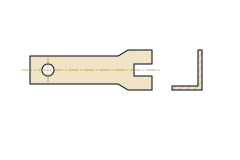
Earth tags, washers, fuse and switch parts and other electrical parts pressed from brass, copper and steel strip.
±0.05 mm on punched features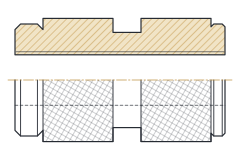
Knurling, broaching, marking and sub-assembly, such as fitting seals into glands before packing.
knurl · broach · mark66 machines: 12 CNC lathes, 20 cam automats, 21 special-purpose machines built in-house, 10 drilling machines and 3 presses.
| Machine type | Qty | Bar or part range | Notes |
|---|---|---|---|
| CNC lathes | 12 | Ø5–100 mm bar | Samples to medium runs; cross-holes and flats in a second operation |
| Cam-operated automats | 20 | Small and medium parts | Bar-fed, long runs |
| Special-purpose machines | 21 | — | Built in-house: turning, drilling, threading, milling |
| Drilling machines | 10 | — | Drilling and tapping |
| Presses | 3 | — | — |
| Process | Parameter | Value |
|---|---|---|
| Turning | Bar diameter | Ø5–100 mm |
| Turning | Part length | ≤ 100 mm |
| Turning | Diameter tolerance | ±0.05 mm |
| Turning | Run-out | 0.05 mm |
| Forging | Part weight | 25 g – 1.0 kg |
| Stamping | Punched features | ±0.05 mm |
| All | General tolerance | ISO 2768-m unless the drawing states otherwise |
Fits tighter than ±0.05 mm: send the drawing; the quote says whether we can hold them.
Materials: CW614N and CW617N as standard; on request low-lead DZR CW511L, lead-free CW724R and DZR CW602N. Grade details
| System | Standard | Typical use | Chart |
|---|---|---|---|
| M | ISO 261 · EN 60423 (glands) | Turned parts, metric cable glands | Metric chart |
| PG | DIN 40430 | Cable glands and accessories | PG chart |
| G (BSP) | ISO 228-1 | Fittings, gland accessories, inserts | BSP chart |
| R / Rc (BSPT) | ISO 7-1 | Tapered pipe fittings | — |
| NPT | ASME B1.20.1 | Fittings for North America | NPT chart |
| UNC / UNF | ASME B1.1 | Inch fasteners and turned parts | — |
| BA / BSW | BS 57 / BS 84 | Older British equipment | — |
Special and customer-specific threads made to drawing. Parallel threads gauged GO / NO-GO.
Nickel, tin and zinc plating is done in our plant; silver and chrome on request. Thickness is measured per lot and recorded on the route card. State the thickness you need in µm in the quote request.
Packed to your specification, with traceable labels (label contents: see Quality).
Pieces per bag, carton weight and pallet type to your specification. Shipping terms: Ordering & shipping.
Send the drawing; if it's outside our range, the reply says so.